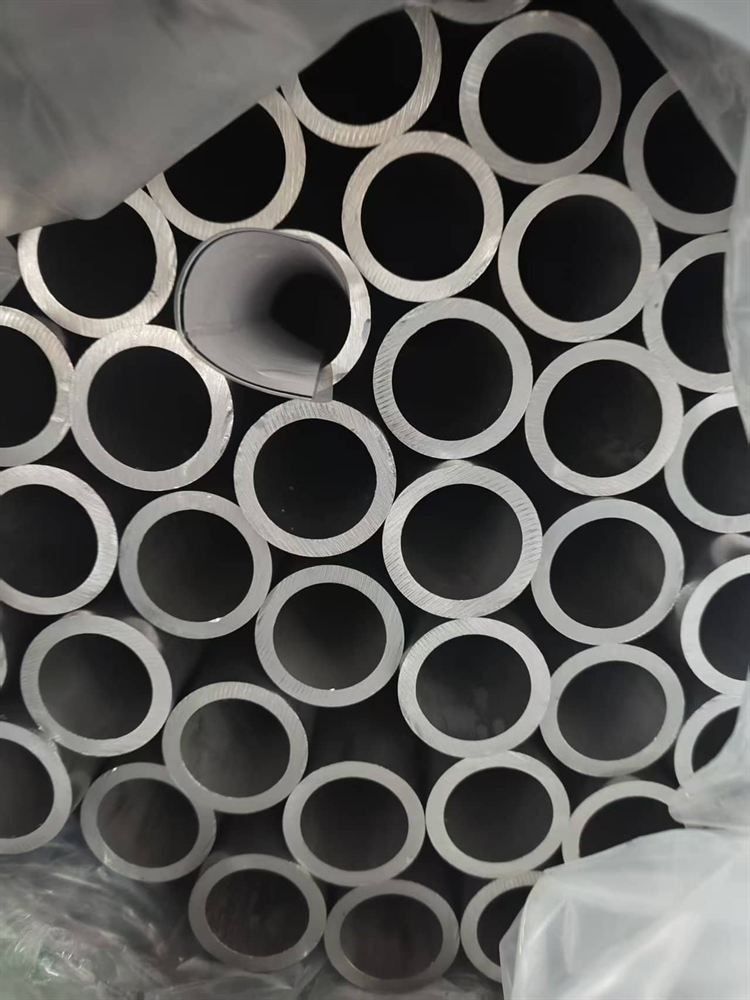
EN 10305-1 E355 Hydraulic Cylinder Tube
Cold drawn seamless tube to EN 10305-1 in grade E355 for hydraulic cylinder barrels. The bore can be supplied honed or skived to a fine finish, so the tube is ready for piston seals without further machining. Wall thickness and straightness are controlled through mandrel drawing.
Price: quoted per specification. Steel prices move with the raw material market, so every quotation is confirmed at the time of order.
Specifications
- Standard: EN 10305-1
- Steel grade: E235, E355, other grades on agreement
- Size range: OD 6-200 mm
- Delivery condition: +C, +LC, +N, +SR
- Production method: Cold drawn, heat treated, honed or skived
E355 against E235
Both grades sit in EN 10305-1 and are drawn the same way; the difference is the guaranteed minimum yield, 355 MPa against 235 MPa. For a cylinder barrel the grade is chosen from bore pressure, wall thickness and the safety factor your customer applies, not from habit. Moving from E235 to E355 normally lets you keep the bore and reduce the wall, which saves weight and material.
Honed or skived bore
Honing uses a rotating, oscillating head and leaves a cross-hatch pattern that holds oil and helps the seal run in. Skiving cuts the bore in one pass and is faster and cheaper on large diameters, but the surface is more directional. Either way the value that matters on the drawing is Ra, not the process name: ask for the Ra your seal supplier specifies and we will confirm which process reaches it on your size.
What to specify in the order
| Item | What to write | If left out |
|---|---|---|
| Bore | Inside diameter after honing, with tolerance | Piston will not fit or fits loose |
| Bore finish | Ra range | Seal wears early, oil weeps |
| Wall | Outside diameter or wall, one of the two fixed | The other dimension is guessed |
| Grade | E355, delivery condition +N or +SR | Hardness may not suit machining or welding |
| Straightness | Deviation per metre, and total over length | Piston binds at the ends of the stroke |
Testing and documents
Chemistry is checked per heat, tensile and elongation per lot, and dimensions, straightness and bore finish by inspection. A hydrostatic test is available on request at the pressure agreed in the order. Certificates to EN 10204 3.1 carry the measured values and the heat number, which is what a cylinder maker needs to close its own inspection report.
Packing and export
Honed bores are the most rust-sensitive surface we ship. Tubes are washed, dried, oiled, plugged at both ends and wrapped before bundling; wooden cases are used where the route or the handling warrants it. Export documents are issued in English with the bore size, length and heat number matching the certificate.
Typical applications
- Hydraulic cylinder barrels
- Pneumatic cylinders
- Honed bore tubes
- Heavy duty actuators
Quality and packing: tubes are protected with anti-rust oil and packed seaworthy, in wooden cases where agreed. Each lot is tested for chemical composition, yield and tensile strength, flattening, elongation and dimensions, with visual inspection and NDT available on request.
Request a quotation: send your size list or drawing through our contact page. We reply within one working day.