ASTM A519 is the American specification for seamless carbon and alloy steel mechanical tubing. It is not a piping standard: the tube is bought for what happens in the machine shop, not for what flows through it. Because it is seamless, the wall is uniform and there is no weld seam to interrupt a bore, a thread or a bearing surface – which is why it is chosen for shafts, hydraulic parts and machined components.
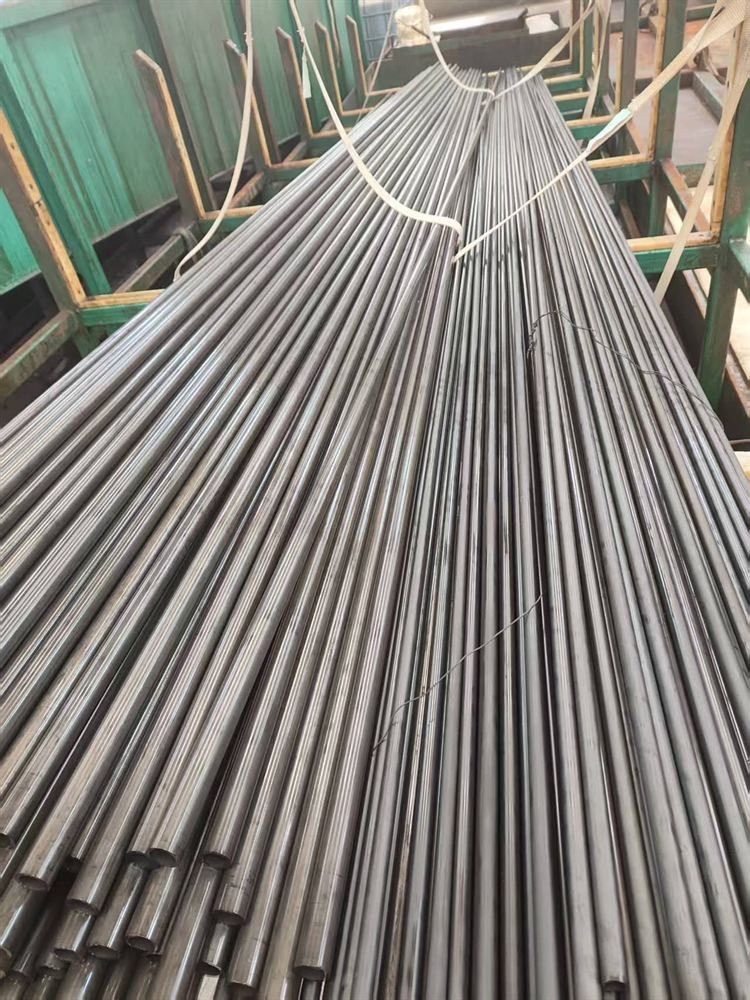
What A519 covers, and what it does not
A519 covers seamless tubing in a wide range of carbon and alloy grades, hot finished or cold drawn, in several delivery conditions. It is the specification behind most “mechanical tube” enquiries: bushing stock, shaft tube, cylinder barrel stock, roller shells, spacers.
What it does not do:
- It is not a pressure piping specification. Pipe for steam, process or transmission lines is bought to A106, A53 or API 5L. An A519 tube can be perfectly sound and still be the wrong document for a pressure line.
- It is not a structural hollow section standard. Welded structural tube is A500; A519 is seamless mechanical tube.
- It does not fix a heat treatment unless you ask. The grade plus the condition define the properties. The same 4140 in the as-drawn and the quenched-and-tempered condition are two different materials.
Grades and what they are for
| Grade | Type | Typical use |
|---|---|---|
| 1010 | Low carbon | General machining, bending, light welding; the default for bushings and spacers |
| 1018 | Low carbon, higher Mn | Better machinability and case-hardening response than 1010 |
| 1020 | Low carbon | Shafts, sleeves, parts that are case hardened |
| 1026 | Medium-low carbon | Higher strength than 1020 at similar machinability |
| 4130 | Chrome moly | High loaded parts after heat treatment: rods, links, suspension and steering components |
| 4140 | Chrome moly | Strength plus wear resistance after quench and temper |
| 8620 | Nickel chrome moly | Case carburised gears, sleeves and wearing parts |
A519 lists many more grades than the ones above – carbon grades through the 1040s and a long list of alloy grades. If your drawing names one we do not hold, ask: availability depends on the mill schedule, not on the standard.
The delivery condition decides the part
| Condition | Effect | Choose it when |
|---|---|---|
| Cold drawn (as drawn) | Highest strength and hardness, lowest ductility, best dimensional accuracy | The part is used as delivered, or strength matters more than machining |
| Cold drawn and stress relieved | Keeps most of the strength, removes the internal stress that makes a bored part move | The tube is machined after delivery – the usual choice for a cylinder barrel |
| Annealed | Softest, most formable, easiest to machine | Heavy machining, forming, or a subsequent heat treatment of your own |
| Normalised | Uniform structure along the length, moderate strength | Parts that need consistent structure rather than maximum strength |
| Quenched and tempered | High strength with usable toughness | 4130 and 4140 parts working under load |
This is the single clause most often missing from an A519 enquiry. Two orders with the same grade and size but different conditions will not machine the same way, and the difference shows up as scrap, not as a complaint.
Mechanical requirements and how they are verified
The standard sets minimum tensile strength, yield strength and elongation per grade and condition, and the mill certificate carries the measured values for the lot. Three practical points:
- Ask for the measured values, not just compliance. If your part is designed to a minimum yield, a certificate that only says “meets A519” does not prove anything.
- Hardness is the fastest check on a delivered lot and the easiest to compare with the certificate.
- For alloy grades, the heat treatment record matters as much as the test result – the same numbers can come from very different cycles.
Tolerances to agree before the order
| Item | What to specify | Effect on the part |
|---|---|---|
| Outside diameter | Nominal and tolerance band | Chucking, collet grip, bearing fit |
| Wall | Nominal and percentage range | Bore size after machining, pressure capacity |
| Inside diameter | Nominal plus allowance where the bore is machined | Whether the finished bore can be reached at all |
| Eccentricity | Maximum wall variation around the section | The reason a thin wall cleans up on one side and not the other |
| Straightness | Deviation per metre | Bar feeder and lathe setup time |
| Length | Fixed or random with a minimum | Cutting loss |
Inspection, testing and documents
| Check | Standard | On request |
|---|---|---|
| Chemistry | Yes, per heat | Product analysis on the finished tube |
| Tensile, yield, elongation | Yes, per lot | Additional tests per heat |
| Flattening | Yes | – |
| Hardness | Common practice | Full-length survey |
| Eddy current or ultrasonic | No | Yes, to an agreed acceptance level |
| Hydrostatic test | No | Yes, at an agreed pressure |
| Certificate | Mill certificate | EN 10204 3.1 |
Cross-reference to the standards you will meet
| Standard | Construction | How it differs from A519 |
|---|---|---|
| ASTM A513 | Welded, some types mandrel drawn | Cheaper; a seam exists, even when drawn |
| EN 10305-1 | Seamless, cold drawn precision tube | European precision tube; tighter dimensional focus, narrower grade list (E215–E355) |
| DIN 2391 | Seamless, cold drawn | Withdrawn predecessor of EN 10305-1, still on old drawings |
| JIS G3445 | Carbon steel tube for machine structures | Japanese grades (STKM), several manufacturing routes including welded |
How to write A519 on a purchase order
“Seamless mechanical tubing to ASTM A519, grade 1020, cold drawn and stress relieved, 60.0 x 10.0 mm, OD tolerance ±0.15 mm, wall ±10 %, length 6000 mm, straightness 1 mm/m, mill certificate with measured tensile and yield, EN 10204 3.1.”
Grade, condition, size, tolerance and document – five items. An enquiry missing the condition is the one that ends in a second order.
Applications
- Shafts and spindles – uniform wall, no seam to interrupt the turned surface.
- Hydraulic cylinder barrels – usually stress relieved before boring and honing.
- Bushings and bearing stock – 1018 and 1020, often case hardened afterwards.
- Rollers, spacers and sleeves – 1010 or 1020 cold drawn, used close to delivered size.
- 4130 structural parts – rods and links after quench and temper.
Frequently asked questions
What is the difference between A519 and A513?
A519 is seamless; A513 starts as welded tube and some of its types are drawn over a mandrel. A513 is cheaper, A519 is specified where a seam is not acceptable or where the part is machined all round.
Can an A519 tube be honed for a cylinder?
Yes, and it is the usual route – but order the stress relieved condition, or the bore will move after the first cut. State the honing allowance so the wall is chosen correctly.
Is 4130 available as drawn?
Yes, but as-drawn 4130 is hard and difficult to machine. Most 4130 parts are ordered annealed for machining and heat treated afterwards, or ordered quenched and tempered to the final property.
Does A519 cover welded tube?
No. If a supplier offers “A519 welded”, the document does not match the product – welded mechanical tube is A513.
Request a quotation: send your size list or drawing through our contact page. We reply within one working day with price, tolerance and lead time.